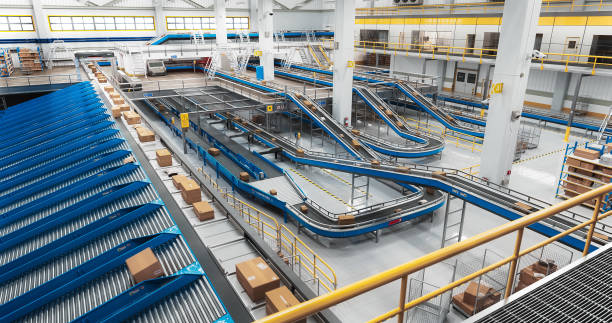
Picture two warehouses shipping the same order volume. One has staff manually reading labels and pushing totes toward the right dock door. The other runs a conveyor sorter that reads a barcode once and routes the item automatically. The second warehouse ships faster, makes fewer mistakes, and does not need to add headcount every time order volume climbs.
MTLI Group has designed and installed sortation systems for Canadian fulfillment operations for more than 40 years. This piece looks at how a conveyor sorter actually works, where it earns its cost fastest, and what operations managers should know before bringing one into a live facility.
Inside the Sort: What a Conveyor Sorter Actually Does
A conveyor sorter reads an identifier, usually a barcode or RFID tag, then physically redirects that item toward a designated lane, chute, or destination using a mechanical device built into the conveyor line. The scan happens once, near the start of the line, and everything after that point runs the routing logic built into the system.
Compare that to manual sorting, where a person reads a label, checks it against a list or screen, and physically carries or pushes the item toward the correct spot. The task is simple in isolation but slows down dramatically the moment volume climbs past what one or two people can keep pace with.
Four Ways a Shorter Routes Product
Sortation equipment comes in several mechanical formats, and the right one depends on product weight, fragility, and how fast items need to move.
| Sortation Mechanism | How It Diverts an Item | Where It Performs Best |
|---|---|---|
| Pop-up wheel or roller | Small wheels rise between belt sections to nudge the item sideways | Light to medium packages, moderate speed lines |
| Sliding shoe | Angled shoes slide across the belt surface to guide items off gently | Fragile or irregularly shaped items needing gentle handling |
| Cross-belt | Individual belt segments tilt and run perpendicular to divert the item | High-speed parcel sortation, dense destination counts |
| Tilt-tray | Trays carrying each item tilt to drop it into a chute at the right point | Mixed-size items, retail and apparel fulfillment |
Facilities handling a mix of product types often run more than one mechanism on the same line, using gentler diverters for fragile goods and faster mechanisms for standard cartons.
The Real Cost of a Mis-Sorted Order
A mis-sorted item does not just cost the price of a reshipment. It costs a customer service call, a return label, and often a damaged reputation with a shopper who now wonders if the next order will arrive correctly. Manual sorting error rates climb noticeably once staff work through peak-hour fatigue or unfamiliar SKUs, and neither problem shows up until a customer complains.
There is also a human cost tied to manual sorting that rarely makes it into a cost-benefit spreadsheet. According to a 2024 release from Canada's Centre for Occupational Health and Safety, 10,211 accepted lost-time injuries related to musculoskeletal and connective tissue disorders were recorded across Canada in 2022, a 2.5 percent increase from the year before. Repetitive lifting and twisting, the exact motions involved in manual sorting, sit near the top of the list of contributing tasks.
Peak Season Is Where Manual Sorting Breaks Down
Order volume rarely grows in a straight line. It spikes around promotions, holidays, and seasonal demand, and a manual sort line built for average-day volume simply cannot flex to match those spikes without a scramble to bring in temporary staff. Statistics Canada's December 2025 payroll data showed couriers and messengers payroll employment up 9.5 percent year over year, with warehousing and storage payroll up 8.3 percent over the same period. Fulfillment demand is growing faster than most facilities can hire for it.
A conveyor sorter does not need overtime approval or a temp agency to handle a volume spike. Once the system is sized correctly, it processes the same throughput on a Tuesday in March as it does during the busiest week of the year.
Sorter Throughput by the Numbers
| Metric | Manual Sorting | Automated Sortation |
|---|---|---|
| Typical sort rate per hour, per line | 60 to 150 items | 3,000 to 12,000+ items, depending on mechanism |
| Error rate under normal conditions | Rises with fatigue and volume | Consistent regardless of shift length |
| Staffing needed to scale for peak | Requires added headcount | Runs at rated capacity without added staff |
| Product handling consistency | Varies by individual worker | Uniform across every item processed |
These figures vary by facility and product mix, but the pattern holds across most fulfillment operations: automated sortation removes the ceiling that a fixed headcount puts on throughput.
Fitting a Sorter into a Facility That Wasn't Built for One
Most conveyor sorters go into buildings that were not originally designed around them, which means the project is as much about integration as it is about equipment. The sorter needs to tie into existing conveyor lines, connect with the racking it feeds into or out of, and often requires reworked dock assignments, so sorted lanes line up with the right outbound trailer.
Because that integration work spans mechanical, electrical, and software disciplines, many facilities bring in a warehouse automation systems integrator rather than trying to coordinate separate vendors for each piece. A single team managing the full scope tends to catch layout conflicts before they turn into an installation delay.
Talking to the Rest of the Building: Sorter and Software Integration
A sorter is only as smart as the routing logic behind it. That logic typically lives in the control software running on the floor, which tells the sorter where each scanned item needs to go based on the order it belongs to, the carrier it ships with, or the zone it's destined for. Without a solid connection between the sorter and that software, the mechanical side of the system has nothing to route by.
Some operations pair sortation with mobile robots for the last leg of the journey, letting a sorter handle the initial split, and robots carry totes the rest of the way to a packing station. Whether that combination makes sense depends heavily on facility layout and SKU mix.
Signs a Sortation Project Is About to Go Sideways
A few warning signs tend to show up before a sortation project runs into real trouble. A vendor who cannot explain how their system will integrate with your existing warehouse software is one. A design that ignores dock door assignments, forcing outbound trailers to load from the wrong end of the building, is another. And a proposal that sizes the sorter for current volume with zero allowance for growth tends to become a bottleneck within a couple of years, the same trap that catches many conveyor projects generally.
Facilities that walk the actual floor with their vendor before finalizing a design, rather than working entirely off drawings, tend to avoid most of these problems before they become expensive.
MTLI's Role in Bringing Sortation Online
MTLI Group designs and installs conveyor sorter systems as part of a broader automation scope that includes structural changes the layout calls for, electrical and controls work, and the crew handling the physical build. That structure means the team responsible for the sorter's design is the same team standing on site when it goes in.
Facilities can review sortation systems we've built for high-volume fulfillment operations across Canada, and every project includes a plan for keeping diverters and belts tuned well after the ribbon-cutting.
Talk to MTLI About a Conveyor Sorter for Your Facility
Manual sorting works fine at low volume, but it runs into a hard ceiling the moment orders climb past what a small team can keep up with. A conveyor sorter removes that ceiling, cuts mis-ship rates, and keeps performing the same way during a Tuesday afternoon lull or a Black Friday rush.
MTLI Group works with fulfillment operations across Canada to design and install sortation systems that fit real order volume, not a generic template. Connect with our design team to talk through your SKU mix and throughput targets.